Epitaxial growth extends a single-crystal lattice only when an atomically clean semiconductor template guides migrating adatoms into step-kink sites. Unlike blanket chemical or physical vapor deposition that yields amorphous or polycrystalline layers, selective epitaxy co-flows chlorinated precursors and HCl etchant so crystalline growth locks onto exposed silicon while dielectric masks remain bare . Whereas material-focused guides examine silicon germanium band structure and strain physics, this article concentrates on lattice continuation criteria, deposition–etch selectivity, and recessed source/drain cavity integration downstream of surface cleaning and source/drain recess .
Physics & Mechanism
Single-Crystal Template Registry and Adatom Kinetics
Epitaxy replicates the underlying substrate's atomic column spacing and crystallographic symmetry across the growth interface . Incoming vapor precursors adsorb and decompose on the exposed semiconductor surface, releasing mobile adatoms that must diffuse to low-energy atomic steps and kink sites before subsequent reactant flux buries them . When surface thermal energy is insufficient or reactant arrival flux outpaces surface migration, adatoms freeze into disordered sites and transition the deposit from single-crystal epitaxy into polycrystalline or amorphous material .
Preserving continuous lattice registry preserves the periodic crystal potential required to minimize mid-gap defect states and carrier scattering in active device regions . In heteroepitaxy—such as growing SiGe or heavily doped silicon alloys on silicon templates—the unstrained lattice-parameter difference defines the lattice mismatch :
Below the critical layer thickness, the growing epilayer deforms elastically to adopt the in-plane lattice spacing of the underlying template, storing coherent strain without forming extended defects . Once accumulated strain energy exceeds the critical threshold, relaxation nucleates misfit and threading dislocations that relieve elastic stress and introduce electrically active recombination paths .
Reversible Chlorosilane Chemistry
Selective epitaxial growth (SEG) restricts crystalline deposition to exposed semiconductor windows while preventing film coalescence on adjacent silicon dioxide or silicon nitride spacers and hard masks . Using chlorosilanes such as dichlorosilane () or silicon tetrachloride () introduces reversible deposition and halogen-etching pathways :
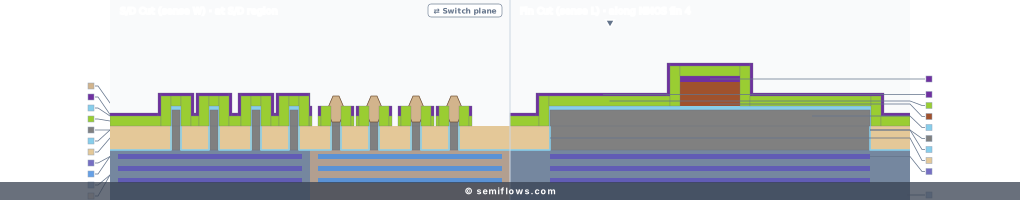
Reviewed course cross-section schematic showing relative layer geometry only; not a physical measurement.
Process checkpoint
Understand SiGe Deposition in context
Inspect the open 28nm selective epitaxial SiGe growth station where single-crystal lattice registry transfers from silicon cavity templates.
Account access is confirmed on the step page.
Selective Co-Flow Kinetics and Cavity Fill Integration
Deposition–Etch Balance, Pattern Dependency, and Faceting
Co-flowing gaseous HCl shifts the surface reaction equilibrium dynamically: nucleation on amorphous dielectric masks requires a higher activation barrier than incorporation onto single-crystal silicon, allowing HCl etchant species to remove disordered adatom clusters from insulator surfaces before a continuous polycrystalline layer forms . Halide surface chemistry also enhances silicon adatom surface mobility, reinforcing selective growth over purely hydride precursors such as silane .
Because net local growth rate equals the balance of vertical and lateral precursor arrival, surface-diffusing species, and HCl etching, selective epitaxy exhibits pronounced pattern dependency and crystallographic faceting . Exposed silicon windows act as reactant sinks; chips or dies with sparse exposed openings draw excess lateral species from surrounding dielectric surfaces, altering both local thickness and alloy composition compared with dense arrays . Simultaneously, slower-incorporating crystal planes (such as faces with fewer kink attachment sites) and asymmetric growth kinetics near dielectric boundaries give rise to faceted epilayer profiles .
Pre-Epi Cleaning and Native Oxide Desorption
Single-crystal registry fails immediately if native silicon oxide, adsorbed moisture-driven re-oxidation, or dry-etch residues remain on the recessed cavity floor . Standard integration pairs ex-situ wet chemical treatments—such as dilute hydrofluoric acid (DHF) to strip native oxide—with rapid transfer into reduced-pressure epitaxial chambers and an in-situ thermal bake or light HCl vapor clean .
In nanoscale recessed cavities and narrow FinFET structures, thermal pre-bake control requires a strict trade-off: sufficient thermal activation must desorb residual interfacial oxide and surface impurities without inducing silicon surface migration, fin height shrinkage, or cavity shape distortion . Low-temperature integrated pre-epi cleaning modules further lower thermal exposure before selective cavity growth begins .
Recessed Source/Drain Filling and In-Situ Doping
Once the recessed cavity presents a clean crystalline template, selective epitaxy grows raised or embedded source/drain structures using chlorinated silicon or germane precursors alongside in-situ hydride dopants such as phosphine () for nFETs or diborane () for pFETs . Operating at reduced pressure transitions growth from mass-transfer-limited transport toward surface-reaction-limited kinetics, curbing boundary-layer autodoping from heavily doped substrates and preserving abrupt junction profiles .
Heavy in-situ doping lowers source/drain series resistance and barrier width for contact metallization, yet faces two coupled limits. First, at elevated dopant concentrations, thermodynamically stable dopant–vacancy complexes (such as clusters) and interstitial formation deactivate a large fraction of incorporated dopants, saturating active carrier density . Second, introducing high dopant partial pressures narrows the selectivity margin against nitride spacers and hard masks, demanding tighter co-flow HCl balance . In dual-epi CMOS flows, subsequent activation anneals must also preserve the elastic strain of previously grown SiGe stressors .
Failure Propagation Chain: Interface Residue to Device Shorting
Selective epitaxy failures propagate across three sequential integration stages when upstream surface preparation or deposition–etch selectivity drifts :
- Upstream Surface and Selectivity Deviations: Incomplete native-oxide stripping, ambient moisture or oxygen re-oxidation during wafer transfer, or etch residues from recess patterning leave partial blocking layers on the exposed silicon cavity . Simultaneously, insufficient co-flow HCl (especially under heavy in-situ doping) fails to strip dielectric-surface nuclei, whereas excessive HCl etchant suppresses or strips growth across exposed silicon cavities and fin sidewalls .
- In-Module Epitaxial Distortions: Residual interfacial oxygen or impurities disrupt step-flow registry, triggering defective nucleation and misfit or threading dislocations that relax epitaxial strain . Imbalanced etchant flux exacerbates non-uniform crystal faceting and eroded fill volume under excess HCl, or leaves unetched adatom clusters that coalesce into parasitic polycrystalline nodules along dielectric spacers and hard masks under weak HCl .
- Downstream Yield and Electrical Failures: Dislocation-induced relaxation collapses uniaxial compressive or tensile channel strain, erasing carrier mobility gains while mid-gap defect states elevate junction leakage . Faceted or under-filled cavities degrade silicide contact landing uniformity and inflate external series resistance, whereas overgrown spacer polysilicon nodules bridge electrically across the gate spacer to short the gate electrode directly to raised source/drain contacts .
Technology Node Evolution and Process Handoff
In planar logic nodes, selective epitaxy shifted from uniform substrate buffers into embedded source/drain stressors inside recessed cavities; the interactive 28nm Planar Flow illustrates this transition directly at its SiGe Deposition station, where exposed cavity walls serve as the crystalline template . You can trace node-specific planar stress coupling and recess geometry trade-offs in selective SiGe epitaxy at 28nm.
As transistors moved to three-dimensional FinFET architectures, selective epitaxy had to fill high-aspect-ratio vertical fins uniformly without parasitic spacer nucleation, forming merged raised source/drain pads before interlayer dielectric deposition, dummy gate replacement, and nickel silicide or cobalt silicide contact formation . Detailed fin-recess and dual-epi integration flows are covered in 14nm selective Si and SiGe epitaxy. Beyond FinFETs, Gate-All-Around (GAA) nanosheet devices rely on blanket epitaxial superlattice stacks followed by inner-spacer definition, selective raised source/drain epitaxy, and selective sacrificial SiGe removal to release suspended channels .
References
(Invited) Selective Epitaxial Growth of High-P Si:P for Source/Drain Formation in Advanced Si nFETs
E. Rosseel, S. Dhayalan, A. Hikavyy, R. Loo, H. Profijt, D. Kohen et al.
State of the Art and Future Perspectives in Advanced CMOS Technology
H. Radamson, Huilong Zhu, Zhenhua Wu, Xiaobin He, Hongxiao Lin, Jinbiao Liu et al. · Nanomaterials
The Challenges of Advanced CMOS Process from 2D to 3D
Henry H. Radamson, Yanbo Zhang, Xiaobin He, Hushan Cui, Junjie Li, Jinjuan Xiang et al. · Applied Sciences
Source/Drain Materials for Ge nMOS Devices: Phosphorus Activation in Epitaxial Si, Ge, Ge1−x Sn x and Si y Ge1−x−y Sn x
A. Vohra, I. Makkonen, G. Pourtois, J. Slotte, C. Porret, E. Rosseel et al.
Silicon VLSI Technology - Full
James D. Plummer, Michael D. Deal, Peter B. Griffin
Silicon VLSI Technology · ISBN 978-0130850379