Within a bounded temperature window and active nucleation sites, atomic layer deposition (ALD) delivers self-limiting, saturation-controlled films . Outside those bounds, precursor thermal decomposition or incomplete purge shifts growth into parasitic CVD , chemically inert surfaces lacking dangling bonds develop sparse island pinholes , while hydrophobic substrates or under-dosed deep trenches suffer delayed closure and thickness gradients. Controlling thermal bounds, surface-site density, and saturation exposure integrates ultrathin high-k gate dielectrics and diffusion barriers across 3D devices .
Core Principles and Manufacturing Significance
Atomic layer deposition operates as a sequential derivative of chemical vapor deposition in which complementary gas-phase reactants never coexist in the chamber at the same time . A canonical thermal ALD cycle alternates four steps—a pulse of precursor AC, an inert-gas purge, a pulse of co-reactant BD, and a second purge—so each half-cycle proceeds only through self-terminating chemisorption and ligand exchange at surface reactive sites . Once every steric-accessible site saturates, additional exposure yields no extra deposition, making thickness track cycle count rather than gas arrival angle .
Whereas an introductory walkthrough of how self-limiting ALD cycles set film thickness explains ideal cycle-by-cycle growth, advanced CMOS manufacturing depends on where that ideal breaks down . As planar MOSFETs transitioned into 3D FinFET and gate-all-around (GAA) nanosheet channels, line-of-sight PVD sputtering suffered view-angle shadowing and poor sidewall step coverage , while continuous CVD faced purity and thickness-uniformity bottlenecks . Integrating ultrathin high-k gate dielectrics (HfO2, depicted below conforming across thin core gate oxide and thick I/O isolation regions) and work-function metal nitrides or carbides therefore requires satisfying three coupled constraints simultaneously: staying inside the precursor temperature window, establishing prompt surface nucleation without island pinholes, and delivering sufficient saturation doses with complete purge separation across high-aspect-ratio structures .
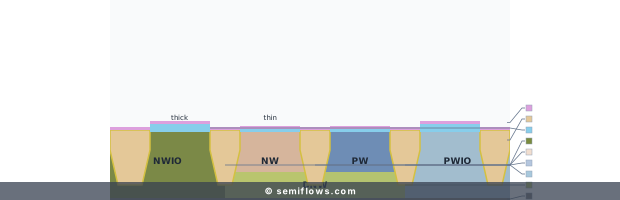
Reviewed course cross-section schematic showing relative layer geometry only; not a physical measurement.
Process checkpoint
Understand High-k HfO2 Deposition in context
Inspect the open 28nm ALD HfO2 gate dielectric station where sequential self-limiting surface reactions control atomic-scale growth.
Account access is confirmed on the step page.
The ALD Temperature Window and Purge Boundary
Self-limiting growth holds only inside a precursor- and co-reactant-specific ALD temperature window . Below the lower thermal bound, surface reaction kinetics lack sufficient activation energy for complete ligand removal, leaving halogen (Cl, I), carbon, or oxygen impurities inside metal-nitride layers such as TiN—elevating film resistivity and shifting effective work function .
Above the upper thermal bound, precursors such as metal alkylamides undergo unimolecular thermal decomposition . Once decomposition supplies reactive fragments independently of surface functional groups, growth shifts into a flux-dependent CVD mode: growth per cycle climbs far above ideal monolayer limits, wafer uniformity degrades, and process variation rises . Even when substrate temperature lies squarely inside the window, an inert-gas purge that fails to separate alternating pulses leaves precursor and co-reactant overlapping in the reaction chamber, triggering the same parasitic CVD loss of control .
Plasma-enhanced ALD (PE-ALD) lowers the required substrate temperature by introducing plasma-activated species instead of relying solely on thermal energy . Compared with directional PVD sputtering—where energetic ions and UV photons break Si–O bonds in the gate dielectric and elevate trap-assisted tunneling leakage—well-controlled PE-ALD uses far lower ion dose and energy; even so, plasma exposure still risks surface damage in delicate gate areas, so thermal ALD remains favored for front-end gate stacks whenever an acceptable thermal precursor route exists .
Surface Nucleation Incubation and Site Density
Linear growth from the very first cycle requires a surface densely populated with reactive nucleation centers . In practical device integration, incoming substrates frequently depart from that state. On chemically inert sp2-bonded surfaces completely devoid of dangling bonds, no continuous nucleation centers exist for ALD precursors to chemisorb ; similarly, substrates with sparse hydroxyl (-OH) functional groups show finite early-cycle incubation , while hydrogen-passivated hydrophobic silicon lacking reactive -OH termination also delays initial chemisorption.
During delayed nucleation, growth initiates only at isolated defect or domain-edge sites, producing sparse three-dimensional islands rather than a compact two-dimensional monolayer . Until islands expand laterally and coalesce, ultrathin high-k dielectrics retain discrete pinholes and elevated gate leakage paths . In work-function metal stacks such as TiN on HfO2, nucleation incubation also produces a compositionally distinct interfacial layer that causes effective work function (EWF) and flatband voltage (Vfb) to shift steeply below a critical thickness threshold . Controlled surface activation, ultrathin nucleation seeds, or amorphous interfacial buffer layers provide dense reactive sites to restore pinhole-free closure, though added interfacial thickness increases equivalent oxide thickness (EOT) and can introduce carrier scattering or doping shifts .
High-Aspect-Ratio Saturation Dose and Integration Constraints
Saturation on an open planar monitor wafer does not automatically hold inside a deep trench, contact hole, FinFET sidewall, or suspended GAA nanosheet cavity. While continuous PVD and CVD suffer line-of-sight view-angle shadowing and sticking-coefficient flux depletion along trench walls , ideal ALD still requires that neutral precursor molecules diffuse to the trench floor and exceed the local saturation exposure threshold during each pulse . Because upper sidewalls consume incoming flux first, deep high-aspect-ratio trenches demand larger precursor exposure integrals to reach full bottom saturation, alongside longer purge steps to clear reaction byproducts out of confined cavities so subsequent pulses do not mix into top-heavy parasitic CVD.
Three-dimensional integration also differentiates thermal ALD from plasma-enhanced and sputtered routes in gate stacks . Thermal ALD delivers uniform 3D FinFET and GAA conformality as well as high-aspect-ratio replacement-gate tungsten gap fill while avoiding the energetic ion and UV Si–O bond damage seen in PVD sputtering and eliminating the plasma surface-damage concern that favors thermal ALD over PE-ALD when temperature allows . Furthermore, in multi-component work-function metal stacks (TiN, TiAlC, or TaAlC), precursor ligand selection, pulse sequence, cycle ratio, and thickness above incubation limits jointly govern Al–C and Ti–C versus Al–N bonding, EWF tuning, and multi-Vt control .
Failure Propagation Chain: Nucleation, Parasitic CVD, and Undersaturation
- Upstream boundary violation (nucleation delay, parasitic CVD, or bottom undersaturation): Chemically inert surfaces lacking dangling bonds , sparse -OH surfaces with multi-cycle incubation , or hydrophobic hydrogen-terminated silicon delay chemisorption and island coalescence; thermal decomposition above the ALD window or incomplete inert-gas purge separation introduces parasitic CVD ; and insufficient exposure integrals in high-aspect-ratio cavities leave deep trench bottoms transport-starved and undersaturated.
- Intermediate film and structural defects (ultrathin pinholes, metal impurities, and thickness taper gradients): Delayed island coalescence traps discrete pinholes in ultrathin high-k dielectrics and incubation roughness or composition transitions in work-function metals , while low-temperature incomplete ligand removal incorporates carbon, oxygen, or halogen (Cl, I) impurities in metal nitrides that raise resistivity and shift work function , alongside structural traps inside gate dielectrics . Simultaneously, upper-wall parasitic CVD or deep-trench bottom undersaturation generates a top-to-bottom thickness taper gradient and thin lower-corner coverage.
- Downstream electrical and barrier failure (gate leakage, Vt drift, and diffusion-barrier breakdown): Pinholes in ultrathin high-k gate dielectrics drive steep gate leakage currents , while dielectric defect traps activate Frenkel–Poole emission, hopping conduction, and percolation-driven dielectric breakdown . Incubation-induced interfacial chemistry variations, fixed charges, and thickness variations shift flatband voltage and effective work function, inducing threshold voltage (Vt) drift . In TiN contact and interconnect liners, discontinuities and bottom-corner thinning compromise diffusion-barrier integrity, permitting aluminum spiking into silicon, chemical interdiffusion, or reactive WF6 precursor attack on underlying titanium and silicides , propagating into contact opens and interconnect failure.
Process Boundaries and Node Evolution
Within the broader thin-film deposition selection map, ALD complements rather than replaces adjacent techniques. Comparing ALD vs. CVD saturation evidence distinguishes genuine self-limiting saturation from continuous CVD or PECVD bulk deposition; directional PVD sputtering shows poor step coverage in narrow vias without collimation or ionization and serves mainly for thick conductive layers over ALD barriers; and FCVD vs. conformal gap fill explains why bulk dielectric trench filling uses flowable deposition rather than slow cycle-by-cycle ALD.
Across technology nodes, ALD expanded from high-k HfO2 gate dielectrics in planar HKMG nodes such as 28nm. Moving into 3D FinFET and GAA nanosheet channels, all-ALD gate stacks—including HfO2, work-function metals (TiN, TiAlC, TaAlC), and replacement-gate tungsten fill—replace directional sputtering and flux-limited CVD .
References
Atomic Layer Deposition (ALD) of Metal Gates for CMOS
Chao Zhao, J. Xiang · Applied Sciences
Atomic-Layer-Deposition Growth of an Ultrathin HfO2 Film on Graphene.
Mengmeng Xiao, Chenguang Qiu, Zhiyong Zhang, Lianmao Peng · ACS Applied Materials and Interfaces
Silicon VLSI Technology - Full
James D. Plummer, Michael D. Deal, Peter B. Griffin
Silicon VLSI Technology · ISBN 978-0130850379