Atomic layer deposition (ALD) grows films one atomic layer at a time by pulsing chemical precursors into the reactor in sequence, letting self-limiting surface reactions do the work: precursor A chemisorbs onto surface sites until saturation stops the reaction by itself, an inert-gas purge clears the chamber, and precursor B reacts with the monolayer left behind — one cycle deposits exactly one layer . Film thickness is therefore set by the cycle count alone, decoupled from deposition time and gas flows; and because growth is driven by surface chemistry rather than line-of-sight or mass transport, every surface inside a deep trench, via, or 3D fin receives the same film. Atomic-scale thickness control, unmatched conformality, and composition precision are what make ALD a cornerstone of nanoscale device manufacturing.
Anatomy of One Cycle: Surface Prep to Finished Film
In production, ALD is never an isolated step: a surface treatment precedes deposition (setting nucleation behavior), and an anneal follows it (densifying the film and stabilizing the interface). The three segments together are the complete story.
- Surface preparation: cleaning and activating the substrate — residual contamination or passivated terminations delay nucleation and skew the first cycles below steady state.
- Self-limiting deposition: precursor pulses alternate with purges; one layer per cycle, thickness uniquely determined by cycle count.
- Post-deposition anneal: densify the film and cut interface state density — turning "the film that grew" into "the film the device works with."
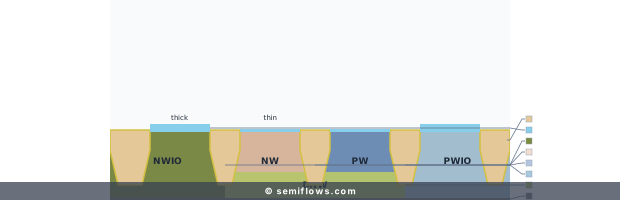
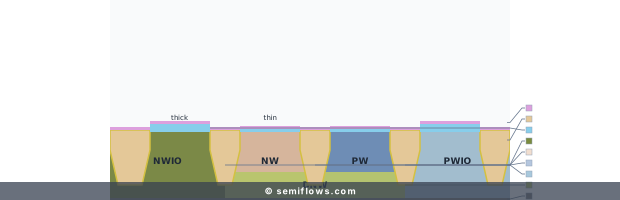
Real cross-sections rendered by the same engine as the 28nm planar course — step names, layer-by-layer rationale, and the full sequence unlock inside the course.
Process map
A selected 3-step learning trail in 28nm Planar Flow
See the surface treatment that prepares reactive sites before high-k deposition — where nucleation begins.
Real step names, layer-by-layer cross-sections, and rationale live inside the 28nm Planar Flow course, unlocked by account access.
Physics & Mechanism
Self-Limitation: The Source of All Control
Precursor A chemisorbs (a strong chemical bond, not physical adsorption) onto reactive surface sites; once every accessible site is occupied, the reaction terminates regardless of further supply. A typical cycle comprises four sequential steps — pulse, purge, pulse, purge . A Langmuir-type surface reaction model explains the self-saturation: steric hindrance from adsorbed species progressively lowers the probability of further adsorption, and the finite density of reactive sites caps growth per cycle. Thermodynamically, the reactions are designed to be strongly favorable on the substrate surface while retaining a high barrier to gas-phase reaction — chemistry happens only where wanted, at the material interface. The purge is the gatekeeper of self-limitation: any precursor left in the gas phase reacts with the next pulse in a CVD-like pathway that destroys the cycle chemistry.
The ALD Temperature Window
Only inside the window do both half-reactions run to completion: too cold and precursor condenses on the surface (liquid-phase reaction, no longer self-limiting); too hot and it decomposes or desorbs prematurely (uncontrolled CVD-like contribution). Within the window, growth is genuinely layer-by-layer — the dividing line between ALD and chemical vapor deposition.
Conformality
Vapor-phase precursor molecules diffuse freely into recessed features; given enough exposure to saturate, tops, sidewalls, and bottoms all receive the same film — something physical vapor deposition (sputtering) cannot do at high aspect ratios because of shading.
Process Principles
- Temperature: inside the window, higher temperature drives half-reactions to completion and reduces residual ligands; below the lower bound reactions stall and condensation threatens, above the upper bound decomposition adds uncontrolled CVD growth.
- Exposure and dose: underexposure leaves sites unreacted and growth low or non-uniform; past saturation, longer pulses no longer change thickness — self-limitation made visible — though some chemistries risk decomposition or co-adsorption on overexposure.
- Purge: insufficient purging opens a gas-phase reaction window (a brief CVD episode that ruins uniformity and traps impurities); more thorough purging improves film quality but costs throughput — every chemistry re-strikes this balance.
- Pressure: lower pressure improves precursor transport to the bottoms of high-aspect-ratio features but reduces surface collision frequency and demands longer exposure; the pressure-exposure interplay is most critical at the most aggressive aspect ratios.
- Precursor chemistry: reactivity, thermal stability, steric bulk, and volatility set growth per cycle, composition, by-product load, and window width — phosphinosilane precursors, for instance, enable low-temperature, damage-free deposition of metal phosphides on sensitive structures.
Challenges & Failure Modes
- Incomplete reaction: low temperature, underexposure, or contaminated sites — growth per cycle drops and varies across the wafer, deep-feature bottoms and wafer centers suffering first.
- CVD-like parasitic growth: above the window or after a poor purge, precursors react in the gas phase; growth becomes a function of time and flow, and uniformity, conformality, and step coverage all degrade.
- Precursor condensation: sub-window temperatures open a liquid pathway — low-density films, trapped ligands, high leakage, fatal for dielectrics.
- Nucleation delay: on inert surfaces the first cycles grow far below steady state, introducing interfacial layers whose composition deviates from the bulk film.
- Impurity incorporation: incomplete purging traps organic ligands in the film — higher resistivity in metals, more interface states and leakage in dielectrics.
- Throughput limits: every layer needs a full pulse and purge sequence, so thick films are inherently slower than CVD — a manufacturing-economics constraint rather than a physical failure.
From Principle to Production Flow
"Surface treatment → self-limiting deposition → post-deposition anneal" appears in production as adjacent, named steps. In the 28nm planar flow's gate module, a dedicated surface treatment precedes the high-k deposition (preparing a reactive interface for the hafnium-based film), the HfO2 atomic layer deposition forms the film, and a post-deposition anneal immediately densifies it. The real step names and layer-by-layer cross-sections live inside the paid course — start from the 28nm planar flow overview to walk to the gate module.
Technology Node Evolution
HKMG stacks entered volume production at 45nm and peaked as the foundry workhorse at the 28nm planar node: ALD deposited the HfO2 gate dielectric (sub-nanometer control, pinhole-free, low EOT) and the TiN/TaN metal gate electrodes that replaced depletion-plagued polysilicon. At the 14nm FinFET node, the FinFET gate wraps three sides of the fin — vertical sidewalls, horizontal tops, and corners must all receive the same thickness, and only ALD's geometry-independent growth delivers; the node's SADP patterning likewise relies on ALD spacer films whose thickness uniformity directly defines the final pitch. At 7nm and beyond, gate-all-around nanosheets demand perfect conformality inside stacked-sheet gaps, and area-selective ALD (AS-ALD) deposits only where surface chemistry permits, replacing some patterning steps with bottom-up growth. In back-end interconnects, ALD liners and barriers occupy a growing volume fraction as features shrink, squeezing the conductive fill — the conformality-versus-conductivity tension driving thinner, more conductive barrier research.
Related Processes
ALD is deeply embedded in its neighbors: pre-deposition surface prep and engineered nucleation layers set the nucleation behavior; SADP/SAQP patterning uses ALD spacer thickness as a lithography variable (see self-aligned quadruple patterning); metal-gate and liner applications hand off to CMP for excess removal; post-deposition anneals must fit ever-tighter thermal budgets; and BEOL MIM capacitors stack ALD precision into higher capacitance density.
Future Outlook
AS-ALD uses self-assembled-monolayer inhibitors for resist-free, bottom-up patterning — critical for plasma-sensitive materials like 2D semiconductors; metal phosphides, 2D materials, and functional oxides expand the materials map; PEALD opens low-temperature pathways with plasma-generated reactants; and molecular-dynamics plus fluid simulations move precursor design from empiricism toward rational engineering. In the era of atomic and close-to-atomic-scale manufacturing, where interfacial quantum effects directly set device behavior, atomistic simulation and process engineering become inseparable.
References
Atomic Layer Deposition (ALD) of Metal Gates for CMOS
Chao Zhao, J. Xiang · Applied Sciences
Silicon VLSI Technology - Full
James D. Plummer, Michael D. Deal, Peter B. Griffin
Silicon VLSI Technology · ISBN 978-0130850379