Photolithography exposes and develops a light-sensitive resist to form a pattern for later transfer. A chip may use many lithography steps, with count and detailed sequence varying by product and layer. This overview uses the named stations in the free 40nm flow as context.
Where Photolithography Acts in the Flow
The 40nm BSI CMOS Image Sensor flow names several lithography stations; three provide examples, with flow cross-section schematics, all publicly visible:
- The first references: an alignment marker photo defines alignment-marker patterns used for registration in later steps.
- Isolation patterning: a shallow trench isolation photo defines the trenches separating neighboring devices.
- The critical layer: a gate formation photo defines a gate resist pattern; the final transistor dimension also depends on transfer and subsequent processing.
Each step is publicly visible with its flow schematic from the 40nm flow overview; the flow is free.
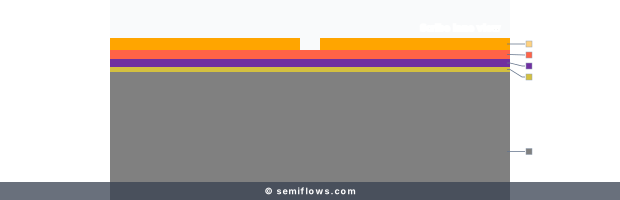
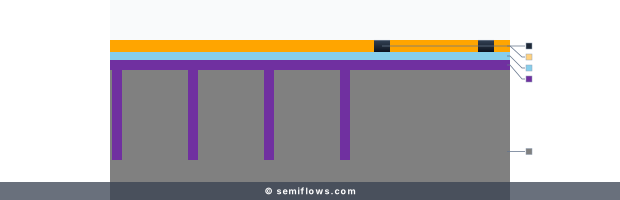
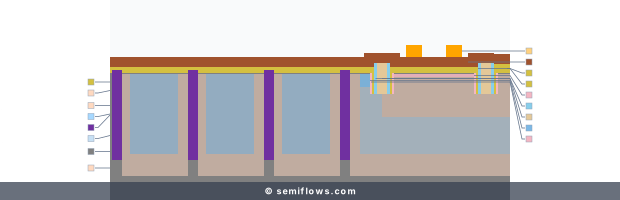
Three named photo stations in the free 40nm flow; schematic patterns do not establish overlay or final dimensions.
Process checkpoint
Understand Gate Formation - Photo in context
Inspect the named Gate Formation - Photo station; the label does not establish final feature dimensions or overlay.
Process context for “Photolithography in a 40nm Process Flow”: 40nm BSI CMOS Image Sensor · GATE · Step 82
Physics & Mechanism
A typical optical lithography step coats resist, aligns a mask or reticle, exposes the resist, and develops a pattern. Bake and pattern-transfer details depend on the resist and flow; some processes use additional layers or repeated exposures . The resist image can guide etch or implantation, but those downstream operations are distinct from the optical exposure itself.
Resolution depends on the imaging system, wavelength, numerical aperture, illumination, mask, resist, and process conditions. Simple scaling relations are useful within specified optical assumptions; they do not set every printed dimension or prove a node from wavelength alone. Overlay describes alignment between layers and has its own error sources. The linked 40nm steps identify alignment marker, STI, and gate photo stations, but do not provide overlay measurements, scanner settings, or a universal minimum feature.
Process Principles
- Separate image from transfer: develop creates a resist pattern; etch or implant uses it in a later operation.
- Check resolution and overlay separately: both depend on the complete imaging and integration sequence.
- Specify the resist: bake and development steps vary with chemistry, including whether a post-exposure bake is needed.
- Use the visible flow as context: its named photo stations do not report process-window measurements.
Challenges & Failure Modes
Focus or exposure variation, overlay error, resist defects, and mask or wafer contamination can affect the printed pattern. Which one limits a product requires measured process windows and defect data. A named gate photo step alone does not prove a specific transistor length.
From Principle to Production Flow
A production flow uses lithography for selected layers, followed by the appropriate transfer or implant operations. The 40nm flow overview provides named photo-station examples and public flow schematics; it does not establish the total exposure count, overlay performance, or exact pattern-transfer result. For related principles, see photoresist, deep ultraviolet, ArF immersion, EUV, SADP, and SAQP.
Technology Node Evolution
Changes in illumination, optics, resist, and patterning strategy have allowed smaller or more complex patterns. A node label does not specify which wavelength or exposure count a particular layer uses; those choices depend on the product and layer.
Related Processes
Photolithography's neighbors: the photolithography walkthrough as the process deep dive; photoresist as the recording medium; EUV, ArF immersion, and deep ultraviolet as the wavelength family; hard mask as the transfer stack; and dry etching as the transfer that consumes what lithography prints.
Future Outlook
Future lithography choices will continue to balance image fidelity, overlay, defects, and cost. Any improvement has to be verified for the intended layer and transfer stack.
References
Silicon VLSI Technology - Full
James D. Plummer, Michael D. Deal, Peter B. Griffin
Silicon VLSI Technology · ISBN 978-0130850379