Introduction
The contact etch stop layer, commonly abbreviated as CESL, is a thin dielectric liner, often silicon nitride, deposited conformally over the transistor gate stack and source/drain regions before interlayer dielectric (ILD) deposition. Its etch-protection role is to serve as an etch-stop barrier during contact hole formation, limiting unwanted removal of underlying isolation or contact-landing materials. Without such a barrier, the anisotropic plasma etch used to open contact holes could penetrate too deeply into the silicon substrate, creating short circuits between adjacent devices or damaging the silicide contact interface.
The intrinsic stress of a silicon nitride liner can also couple into the transistor channel and modify its electrical response. The film’s etch-stop role and its possible stressor role must be assessed separately: a CESL label alone does not prove improved mobility, and the transfer depends on device geometry and layout .
Process checkpoint
Understand CESL 1 - Deposition in context
Inspect the open 40nm PECVD SiN CESL deposition step protecting active junctions during oxide contact etching.
Account access is confirmed on the step page.
Physics & Mechanism
Stress Generation in PECVD Silicon Nitride
CESL films are typically deposited by plasma enhanced chemical vapor deposition (PECVD) using precursor gases such as silane (SiH₄) and ammonia (NH₃), diluted in a carrier gas. The plasma dissociates these precursor molecules into highly reactive radicals — SiHₓ, NHₓ, and atomic hydrogen — which react at the wafer surface to form an amorphous hydrogenated silicon nitride film (a-SiₓNyHz). The film's intrinsic stress is determined by the bonding structure established during deposition: the ratio of Si–H, N–H, and Si–N bonds, the film density, and the ion bombardment energy from the plasma all contribute to whether the film is in a state of compressive or tensile stress.
Deposition and subsequent treatment can change composition, hydrogen bonding, density and stress. These properties are coupled and do not follow a universal rule based on gas ratio or power alone . The reviewed SiNx examples report increased tensile stress after ultraviolet/thermal treatment associated with hydrogen removal, but that observation is bounded by the initial film and treatment; it is not proof that UV always improves a transistor or that N–N bonding is thermodynamically impossible .
Stress Transfer to the Channel
A mechanism by which a stressed CESL can affect transistor performance is stress transfer through elastic mechanical coupling. According to Hooke's law and elasticity theory, a film under intrinsic stress exerts a force on the substrate to which it adheres. In a MOS transistor, the CESL covers the gate stack, spacers, and source/drain regions conformally. The stress in the film is transferred into the silicon channel through the gate structure and the sidewall interfaces.
Channel strain changes the electronic band structure and carrier transport, but the response depends on crystal orientation, transport direction, strain components and operating condition. Tensile liners for nMOS and compressive liners for pMOS are established examples, not a universal mapping from the sign of film stress to mobility gain. The cited reviews describe layout-dependent responses .
A film-stress measurement, channel-strain measurement and transistor current measurement answer different questions. Even when mobility improves, total drive current still depends on series resistance, electrostatics and bias. Do not convert a film stress value directly into an Ion/Ioff improvement .
Etch Selectivity Chemistry
Etch selectivity is the ratio of removal rates under the same specified conditions. In one contact scheme, oxide is removed preferentially while enough nitride remains to protect the underlying region; a later operation opens the nitride locally. Fluorocarbon surface-film formation and removal contribute to oxide/nitride selectivity. SiN can also etch and form fluorinated products, so the boundary is neither automatic nor loss-free .
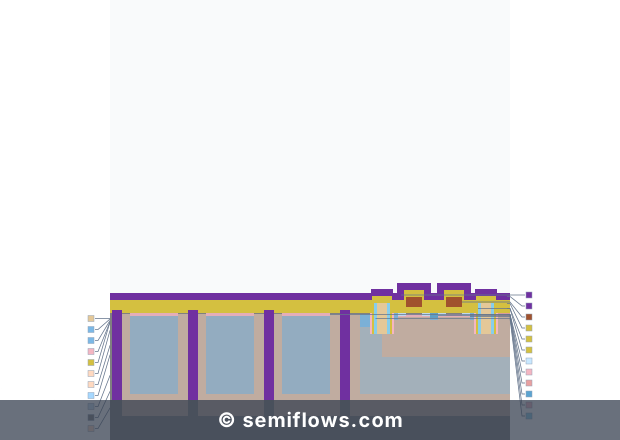
Reviewed course cross-section schematic showing relative layer geometry only; not a physical measurement.
Process Principles
Deposition Parameter Effects on Stress
Deposition settings alter coupled film properties. Interpret trends within the measured deposition system rather than treating each setting as an independent stress control :
-
Gas composition: changes in Si/N ratio and hydrogen incorporation can change bonding and stress; “more silicon” does not specify a universal stress sign.
-
Plasma conditions: energy and flux affect growth and surface interaction. Density, composition and stress can change together, so power alone does not uniquely determine ion energy or film stress.
-
Temperature: reaction kinetics and hydrogen retention can change with temperature, while the existing device stack constrains the thermal budget.
-
Post-deposition treatment: the cited UV/thermal examples increase tensile film stress, but the film response and final device response must be checked separately .
Geometry and Stress Transfer Efficiency
The efficiency of stress transfer from CESL to the channel is strongly influenced by device geometry. Key geometric factors include:
-
Gate and contact spacing: spacing changes stress transfer and relaxation. In the layout examples reviewed in , wider poly spacing could increase channel stress toward saturation, while a nearby contact opening could relax the liner. This contradicts a blanket rule that tighter spacing always amplifies stress.
-
Gate and spacer geometry: the shape and mechanical boundary conditions alter the strain distribution. Taller gates or more sidewall area do not by themselves establish a larger useful channel-strain component.
-
Film thickness and patterning: thickness contributes to the mechanical load, but later openings change continuity and allow local relaxation. The stress in a blanket film is not the final patterned-channel strain .
Etch Selectivity Integration
Different ILD thicknesses and local etch rates can cause openings to reach the CESL at different times. The early-arriving locations consume stop-layer margin while other locations continue clearing. The CESL provides a finite over-etch budget; it does not synchronize arrival or guarantee that every contact simultaneously exposes silicide .
The local CESL-opening operation has its own removal and damage limits. Its landing surface may be semiconductor, pad oxide, or an existing contact layer, depending on the integration sequence. In the linked open 40nm flow, CESL opening precedes pad-oxide removal, cleaning, and Ti/TiN/W contact metallization, so it must not be described as opening an already completed plug.
Challenges & Failure Modes
Stress Relaxation and Non-Uniformity
Later processing can change hydrogen content, bonding and stress in a PECVD film. Outgassing, peeling or cracking are possible and depend on the film and conditions . A change in film stress can alter the intended channel strain; neither relaxation nor a shift toward tension is universal for every thermal step.
Non-uniform stress distribution across the wafer is another concern. Variations in PECVD plasma density, gas flow distribution, and temperature uniformity can create spatial stress gradients, leading to device-to-device variability in drive current and threshold voltage. The resulting device response must be evaluated with its layout and operating conditions .
Contact Resistance and Parasitic Effects
An intact dielectric CESL is not a desired series-resistance element inside the conductive contact: it must be opened at the intended contact location. Residual dielectric can obstruct current injection. Low-resistance semiconductor contacts also depend on interface barrier, active doping and current transport . Removing residues and preserving the landing material are separate requirements; no one wet-clean/O₂-ash sequence is established for every contact by the CESL name.
Adhesion and Delamination
CESL films under high intrinsic stress (whether tensile or compressive) are susceptible to adhesion failures. If the interface between the CESL and the underlying spacer or ILD is weak, the film stress can cause delamination, creating voids or blisters that compromise both the etch-stop function and the strain transfer mechanism. Gas incorporation and later outgassing can also contribute to film failure, depending on the deposited material and subsequent conditions .
Process Window Constraints in Advanced Nodes
Thinner local regions leave less material to consume during etching, while film thickness, coverage, stress and available space constrain one another. These are stack-specific trade-offs, not a rule that each node must use a thinner CESL. Assess local remaining thickness and contact clearance separately from any proposed strain benefit.
Connect the Mechanism to a Named Step
The linked open 40nm flow places CESL 1 - Deposition (PECVD silicon nitride) at Step 105 ahead of a second CESL liner and multi-stage PMD oxide fill. Even where ALD nitride studies demonstrate why coverage and wet-etch resistance must be evaluated separately , Step 105 serves here as an etch-protection and stress-context boundary before PMD fill without certifying dual-stress mobility gain. Use the station to identify the deposited nitride layer and sequence boundary, not to infer a universal node mobility gain or deposition ranking.
The interaction between CESL and adjacent operations must be checked in the actual flow. The contact hole etch process must be co-designed with the CESL material to ensure that the etch-stop function is reliable across all contact locations, while the break-through etch step that removes the CESL over the source/drain must achieve complete removal while limiting loss or damage of the actual landing material.
Related Processes
CESL does not exist in isolation; it is intimately connected to several adjacent process steps in the middle-of-line (MOL) and back-end-of-line (BEOL) integration sequence.
Contact Hole Etch
The most direct relationship is with the contact hole etch process, which relies on the CESL as an etch-stop boundary. The two-step etch — oxide etch stopping on CESL, followed by local stop-layer opening to the intended landing surface — is a fundamental integration scheme. The etch chemistry, selectivity ratios, and process window must be jointly optimized for the specific CESL material used. Related processes such as reactive ion etching provide the anisotropic etching capability that makes this selective etch possible.
ILD Deposition and CMP
ILD fill and later CMP determine the incoming topography and material exposure for subsequent operations. A CESL is not automatically a CMP stop: exposure, relative removal rates and the actual endpoint determine whether it is consumed or retained. Film compatibility and mechanical integrity remain integration constraints .
Salicide Formation
The position of silicidation or contact interface formation relative to CESL is flow-dependent. When an existing silicide lies beneath the film, deposition and thermal processing must preserve the required interface. In the linked 40nm sequence, pad-oxide etch, cleaning, and Ti/TiN/W contact deposition follow CESL opening; do not assume an earlier flow's salicide order applies to every integration.
Post-Etch Residue Removal
Post-etch cleaning addresses the residue species left by the actual etch while preserving the landing material and protective dielectric. Carbon-containing films and damaged interfaces are different problems. The related post-etch residue removal topic describes the cleaning task; it does not make one named cleaner mandatory for every CESL opening.
References
Silicon VLSI Technology - Full
James D. Plummer, Michael D. Deal, Peter B. Griffin
Silicon VLSI Technology · ISBN 978-0130850379
Physics of Semiconductor Devices - Full
S. M. Sze, Kwok K. Ng
Physics of Semiconductor Devices · ISBN 978-0-471-14323-9
Study of the SiO2-to-Si3N4 etch selectivity mechanism in inductively coupled fluorocarbon plasmas and a comparison with the SiO2-to-Si mechanism
M. Schaepkens, T. Standaert, N. R. Rueger, Pgm Patrick Sebel, G. Oehrlein, J. M. Cook
State of the Art and Future Perspectives in Advanced CMOS Technology
H. Radamson, Huilong Zhu, Zhenhua Wu, Xiaobin He, Hongxiao Lin, Jinbiao Liu et al. · Nanomaterials
Physical, Electrical, and Reliability Considerations for Copper BEOL Layout Design Rules
E. Shauly · Journal of Low Power Electronics and Applications
Atomic Layer Deposition of Wet-Etch Resistant Silicon Nitride Using Di(sec-butylamino)silane and N2 Plasma on Planar and 3D Substrate Topographies.
T. Faraz, M. van Drunen, H. Knoops, A. Mallikarjunan, Iain Buchanan, D. Hausmann et al. · ACS Applied Materials and Interfaces