Scaling EOT in HKMG stacks hinges on controlling the interfacial-oxide floor, thermal regrowth, and oxygen-vacancy dipoles rather than permittivity alone. Because an ultrathin lower-permittivity interfacial layer sits electrically in series with the overlying high- film, post-deposition oxygen diffusion and defect dipoles dictate real capacitance scaling and threshold stability . Whereas our foundational EOT calculation guide defines ideal series formulas and our CET boundary checklist audits measured capacitance conventions, this article details the HKMG scaling bottlenecks connecting interfacial chemistry to HKMG gate-stack reliability .
Physics & Mechanism
Interfacial Oxide Series Capacitance Floor
In a practical -based gate stack, total dielectric equivalent oxide thickness combines the electrical contributions of the high- layer and the underlying silicon oxide or oxynitride interfacial layer (IL) in series :
Even when a high- dielectric achieves large permittivity with sufficient physical thickness to exponentially suppress direct quantum tunneling , the lower-permittivity IL acts as a hard series capacitance floor . Simply removing the IL on hydrogen-terminated silicon (H/Si) fails in standard water-based ALD flows because hydrophobic H/Si surfaces lack reactive hydroxyl nucleation sites, producing delayed island growth, discontinuous films, and excessive leakage . Moreover, placing high- oxides directly on silicon heightens interface defect density, remote soft-optical-phonon scattering, and fixed-charge Coulomb scattering that degrade channel carrier mobility .
Dielectric EOT vs. Measured Inversion CET
Device measurements extract capacitance in strong inversion rather than probing the dielectric stack in isolation . Consequently, measured capacitance-equivalent thickness (CET, denoted in MOS capacitor theory) includes semiconductor and electrode series capacitances alongside the insulator EOT :
Here represents polysilicon gate depletion under inversion bias and captures the finite quantum-mechanical centroid depth of the channel inversion charge inside silicon . Replacing doped polysilicon with a metallic gate eliminates () and stops boron penetration , yet quantum-mechanical inversion-layer capacitance () persists . Mixing dielectric-only EOT with inversion CET confounds dielectric thickness assessment unless the capacitance boundary is explicitly separated in CET vs. dielectric EOT.
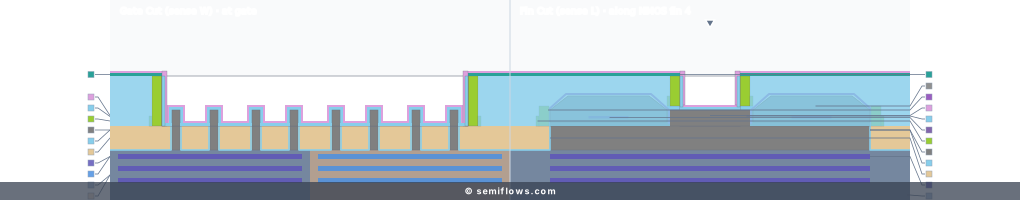
Reviewed course cross-section schematic showing relative layer geometry only; not a physical measurement.
Process checkpoint
Understand High-k HfO2 Deposition in context
Inspect the curated high-k HfO2 gate dielectric station enabling lower EOT without thin-oxide tunneling breakdown.
Account access is confirmed on the step page.
HKMG Scaling Bottlenecks: Regrowth, Crystallization, and Dipoles
Thermal Interfacial Layer Regrowth Control
Although ALD hafnium dioxide avoids severe silicide reactions with silicon, post-deposition annealing (PDA) and high-temperature dopant activation expose the gate stack to oxygen transport that regrows the bottom IL . Oxygen arrives both from oxidizing anneal ambients diffusing rapidly along high- grain boundaries and from residual atomic oxygen stored inside refractory metal electrodes such as tungsten or rhenium .
Because every incremental unit of regrown adds its full thickness directly to EOT, suppressing regrowth is as critical as thinning the deposited high- film . Integration counters IL regrowth either by using oxygen-diffusion barrier electrodes such as TaSiN to minimize interfacial thickening , or by adopting replacement metal gate (gate-last) sequences that execute high-temperature source/drain dopant activation before depositing work-function metals such as pMOS TiN , avoiding both refractory-metal residual-oxygen oxidation and metal-gate work-function instability, as mapped in HKMG integration order .
High-k Crystallization and Amorphous Stabilization
Pure transitions from an amorphous deposit into a monoclinic polycrystalline film under elevated thermal processing . While grain boundaries accelerate oxygen indiffusion toward the channel interface , optical and electrical spectroscopy show that crystalline also generates localized band-edge defect states that sustain Frenkel–Poole trap-assisted hopping conduction and introduce grain-to-grain threshold and leakage variability as gate lengths shrink .
Alloying with silicon and nitrogen () raises crystallization stability and reduces remote phonon scattering relative to pure , while nitrogen increases permittivity and impedes boron or oxygen diffusion . However, this creates a spatial placement constraint: nitrogen located near the top of the dielectric improves EOT scaling cleanly, whereas nitrogen penetrating close to the silicon channel introduces positive fixed charge that shifts flatband voltage and degrades mobility via Coulomb scattering .
Oxygen-Vacancy Dipoles and Vfb–EOT Roll-Off
Setting symmetric, low threshold voltages requires tuning effective work function (EWF) rather than relying on vacuum metal work functions alone . Under moderate thermal budgets or reducing ambients, high-workfunction metal gates adjacent to drive charged oxygen-vacancy formation () with electron transfer into the gate, creating an interfacial dipole layer that pulls effective work function and back toward midgap .
When the bottom interfacial layer is aggressively thinned, devices exhibit severe –EOT roll-off: mechanical stress in the transitional sub-oxide drives oxygen out-diffusion from the bottom interface into the high- stack, generating interfacial defects and accelerating work-function drift especially on pFET stacks . Suppressing this drift combines stress-relieved thermal pre-oxides , robust interface bonding passivation , controlled oxidizing/fluorine defect passivation , and dielectric dipole capping layers that shift band offsets without thickening the IL .
Failure Propagation Chain: Interface Instability to Threshold Mismatch
EOT scaling failures in HKMG stacks propagate along two competing thermal-and-interface pathways into a unified device-level breakdown :
- Upstream Interface and Thermal Deviations: Pushing the interfacial layer too thin on poorly functionalized or unpassivated silicon surfaces compromises chemical bonding and ALD nucleation ; conversely, excessive post-deposition thermal exposure or unsealed oxidizing ambients drive inward oxygen diffusion through high- films or out of refractory electrodes .
- In-Stack Dielectric and Electrostatic Distortions: Under-passivated, stressed ultrathin ILs accumulate high interface trap density () and undergo oxygen out-diffusion that nucleates charged oxygen-vacancy dipoles, causing –EOT roll-off and trap-assisted tunneling . In the opposite regime, oxygen indiffusion regrows a thicker low- IL that causes EOT to rebound while high thermal budgets crystallize , generating grain-boundary leakage pathways and band-edge charge traps .
- Downstream Transistor Drive and Threshold Failures: Rebounded EOT combined with Coulomb and remote-phonon scattering lowers inversion capacitance and carrier mobility, degrading transistor drive current . Simultaneously, dipole-driven drift and polycrystalline grain heterogeneity induce severe threshold voltage mismatch across nFET/pFET arrays, while percolative defect accumulation accelerates gate leakage runaway and NBTI/PBTI reliability wear-out .
Technology Node Evolution and Process Context
When planar CMOS reached the 45nm node, conventional silicon oxynitride hit its direct-tunneling scaling ceiling, driving mass production of /metal gate stacks . This planar HKMG architecture carries forward to the integrated flow illustrated in the 28nm Planar Flow (High-k HfO2 Deposition station), showing how high-permittivity dielectric formation builds on thermal gate oxidation and pairs with titanium nitride work-function metal engineering ; for a deeper contrast between capacitance and tunneling transport, consult capacitance is not leakage .
Transitioning to 3D FinFETs and stacked Gate-All-Around (GAA) nanosheets shifts the primary physical constraint from planar thickness uniformity to atomic-scale conformality and low-damage thermal ALD . Sputtered metal gates suffer shadowing and plasma damage on vertical fin sidewalls and horizontal nanosheet cavities, making conformal ALD high- dielectrics and ALD work-function metals—paired with oxide densification and dual gate oxide isolation across core and I/O domains—essential to keep EOT and effective work function uniform around every crystal facet of the channel .
References
Advanced high-k dielectric stacks with polySi and metal gates: Recent progress and current challenges
E. Gusev, V. Narayanan, M. Frank · IBM Journal of Research and Development
The Progress and Challenges of Applying High-k/Metal-Gated Devices to Advanced CMOS Technologies
H. Tseng
Atomic Layer Deposition (ALD) of Metal Gates for CMOS
Chao Zhao, J. Xiang · Applied Sciences
Modern Semiconductor Devices for Integrated Circuits - MOS Capacitor
Chenming Hu
Modern Semiconductor Devices for Integrated Circuits · Ch5 MOS Capacitor
Silicon VLSI Technology - Full
James D. Plummer, Michael D. Deal, Peter B. Griffin
Silicon VLSI Technology · ISBN 978-0130850379