Process Map and Scope
A 7nm FinFET process flow connects fin formation, transistor gates, source/drain regions, contacts, and metal wiring into a working CMOS circuit. Its central integration problem is to preserve device control and reliable connections as structures become small and closely spaced. Lithography, etch, deposition, cleaning, and chemical mechanical polishing (CMP) act on the same evolving structure, so each module must leave a usable input for the next. The textbook discusses these general fabrication operations and their integration .
The node name does not specify one universal lithography sequence. For example, TSMC's N7+ announcement distinguishes its EUV-enabled N7+ process from the original N7 generation. That distinction does not establish that every 7nm contact or metal layer uses EUV. The interactive flow discussed here is a teaching sequence: its fin-patterning section includes SAQP, its gate section includes SADP, and its metal sections identify lithography and etch handoffs. A step named M10 Lithography alone does not identify an exposure technology or a minimum metal pitch.
The useful process map separates three tasks. Front-end-of-line (FEOL) modules form and control the transistor; middle-of-line (MOL) modules connect its terminals; back-end-of-line (BEOL) modules build the wiring network. This article explains their physical dependencies. Commercial implementations can differ in materials, patterning choices, and module boundaries.
Process map
7nm FinFET
Understand the integration logic and module handoffs across the 7nm FinFET.
Public flow overview
Major Modules and Dependencies
FEOL: Fin Formation, Isolation, and Gate Definition
Fin geometry determines the channel surfaces that the gate can control. In the teaching flow, spacer-based pattern multiplication and hardmask transfer precede the silicon pattern transfer and isolation sequence. Spacer formation can create closely spaced features, but the final fin profile also depends on transfer etches, mask integrity, and subsequent processing. Pattern multiplication is therefore a chain of dimensional handoffs, rather than an automatic guarantee of uniform fins.
Isolation separates neighboring active regions while leaving the intended fin surfaces available for later transistor processing. Deposition, CMP, and recess steps must be considered together: fill quality and surface height influence the geometry seen by the gate module. The sequence shown in this flow is one concrete learning example; it does not make the relative ordering of fin formation and well engineering a universal rule for all FinFET processes.
The gate-stack integration module provides the next connection. A dummy gate establishes an intermediate structure, and replacement-gate processing later prepares and fills the gate cavity. Cleaning and removal must preserve adjacent materials, while the final dielectric and metal stack must provide the intended electrical behavior.
Source/Drain and Epitaxy
The source/drain module connects channel geometry to current delivery. Epitaxy, doping, and the resulting interfaces affect carrier transport and access resistance. Strain can modify carrier transport, but its effect depends on material, geometry, and the stress actually transferred to the channel. A node label alone does not establish a particular dual-width-fin design or prove that a change improves both electrostatics and resistance.
The integration question is what the gate, spacer, and fin structure allow the source/drain steps to change. Processing that improves one interface can also alter junction shape, consume material, or expose another region to damage. The module must be studied with those neighboring structures in view.
MOL: Contact Formation
Contacts connect the transistor terminals to the wiring network. Their electrical performance depends on opening geometry, the condition of the contacted surface, and the materials at the interface. Contact formation must remove the intended dielectric while protecting nearby structures; a correctly placed opening can still make a poor connection if residue or damage remains at its bottom.
Lithography influences the opening geometry, but it does not independently determine contact resistance. Choosing EUV for a particular layer may reduce some patterning steps; it does not eliminate dimensional variation, etch error, or interface resistance. Imec's patterning review identifies stochastic roughness and failures in EUV-patterned resist as continuing concerns.
BEOL: Interconnect Construction
BEOL processing forms metal lines and the vias connecting successive levels. In a copper damascene sequence, openings are patterned in dielectric, prepared for metallization, filled, and planarized. The textbook source explains why copper deposition into dielectric openings followed by CMP avoids the need to pattern the copper by a conventional subtractive plasma etch .
Different wiring levels can have different roles and geometries. Neither the 7nm label nor a metal-level number establishes which layers use EUV, whether a layer is at minimum pitch, or whether cut and dummy features can be removed. The relevant learning question is how each level receives the preceding surface and delivers a usable one to the next.
Device Physics and Integration Logic
Electrostatic Control and Short-Channel Effects
A FinFET gives the gate control over multiple channel surfaces. The purpose is to limit the drain's influence over the channel potential as device dimensions shrink. Fin shape, gate dielectric, gate geometry, and junction structure all participate in that control. Better electrostatics must still be reconciled with current delivery, leakage, and variability.
Fin width is one of those interacting variables. It affects the channel geometry, but a statement about one width or one device simulation cannot define every production implementation. The cited double-gate FinFET study examines work-function and geometry effects in a modeled device; it is useful as an illustration of interacting electrical variables, rather than as a 7nm manufacturing specification .
Gate Stack and Work Function
Gate dielectric and metal choices affect the relationship between applied gate bias, channel charge, and threshold voltage. The cited simulation studies changes in metal-gate work function and reports corresponding changes in device characteristics . That supports the principle that work function is an electrical design variable; it does not prove that multiple threshold-voltage options are introduced without any performance or variability cost.
In the replacement-gate sequence, cavity preparation, dielectric interfaces, and metal fill must all remain consistent with that electrical objective. The dummy-poly opening and planarization module is useful for examining the intermediate surface and cavity that later gate processing receives.
Resistance, Capacitance, and Pattern Transfer
Current flows through a chain of transistor regions, contacts, vias, and metal lines. Resistance in any link can reduce the benefit of improving the channel alone. Nearby conductors also couple through dielectric, so geometry and material choices influence capacitance as well as resistance. The textbook discusses interconnect resistance, capacitance, and electrical measurements as related BEOL concerns .
A patterning change should therefore be evaluated at several handoffs: the resist image, the transferred opening, the filled conductor, and the measured electrical structure. Simplifying the exposure sequence does not guarantee that all four improve. Cleaning, etch profile, barrier continuity, fill quality, and CMP can change the final result.
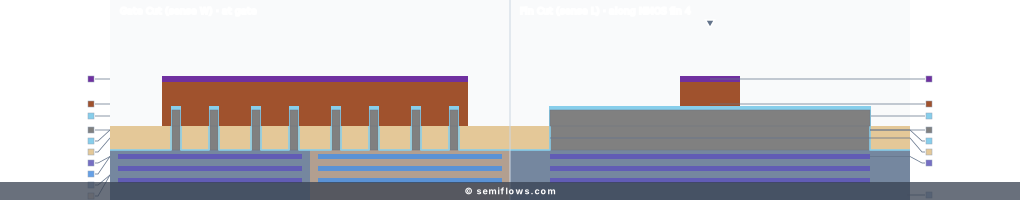
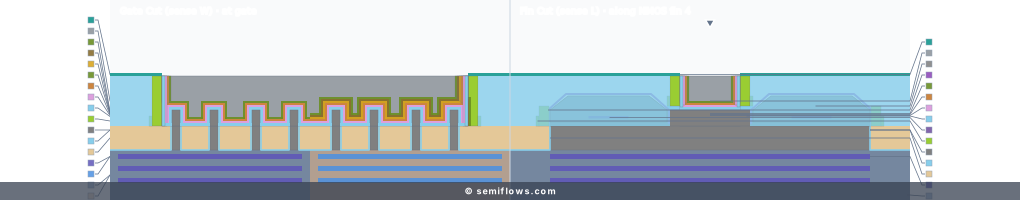
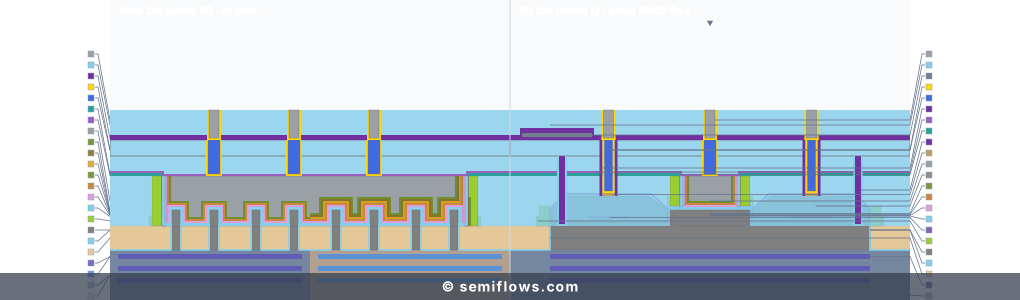
Schematic 7nm FinFET integration cross-section illustrating dual Gate Cut and Fin Cut geometry; quantitative process conditions are intentionally omitted.
Interface Risks and Failure Propagation
Dimensional handoffs: Spacer thickness variation, mask transfer, overlay, and etch can change feature placement or shape. EUV has its own resist roughness and stochastic failure concerns, so an EUV label cannot serve as proof that contact or interconnect variation has disappeared.
Fin and gate interfaces: A change to fin shape or an adjacent surface can alter the structure seen by later epitaxy or gate processing. Removal and cleaning steps must preserve the regions that are intended to remain.
Contact interfaces: Residue, incomplete opening, or damage at the contact bottom can impair the connection even when the top-view pattern appears acceptable. Protection of nearby gate and source/drain structures remains a separate requirement from lithographic placement.
Metal fill and planarization: Discontinuous preparation layers, incomplete fill, or excessive material removal can produce resistance, leakage, or topography problems. The textbook distinguishes metal dishing from dielectric erosion during CMP and explains why surface topography matters to later processing .
Thermal history: Heating affects dopant activation, diffusion, and material interfaces. Later steps inherit structures already formed earlier, so their thermal requirements must be considered together. General diffusion and implantation principles provide a way to reason about this interaction without turning the teaching flow into a manufacturing recipe .
How to Study the Interactive Flow
Use the flow overview to identify module boundaries, then trace one intermediate structure through its upstream and downstream steps. For each handoff, ask what material is present, which surface or opening must change, which region must survive, and what electrical function depends on the result.
Three useful paths are the gate stack, source/drain integration, and dummy-poly opening and planarization. They connect device-control questions to the structures that the teaching sequence actually presents. The learning route accompanying this article opens the 7nm flow overview, so readers can choose a module before entering an individual step.
Scope and Transfer to Other Generations
The transferable lesson is to follow geometry, interfaces, and electrical function across module boundaries. Changing transistor architecture or patterning technology changes parts of that network, but it does not remove the need to prepare contacts, manage material interfaces, or deliver reliable wiring.
The official N7+ example establishes that EUV adoption belongs to a particular platform history. The textbook and modeled-device references establish general mechanisms within their own scope. The interactive sequence supplies a concrete teaching topology. Reading those three kinds of evidence together helps explain a 7nm FinFET process flow without treating them as one universal commercial process.
References
Silicon VLSI Technology - Full
James D. Plummer, Michael D. Deal, Peter B. Griffin
Silicon VLSI Technology · ISBN 978-0130850379
Performance evaluation of novel low leakage Double-gate FinFET device at sub-22nm with LaAlO3 high-k gate oxide and TiN metal gate using quantum modeling
S. Subramaniam, Sangeeta Joshi, R. Awale · International Conference on Electronics, Circuits, and Systems